Quick Answer
Cutting tool pretreatment before coating improves tool life by preparing the substrate so the coating bonds to a cleaner, more uniform, and more mechanically stable surface. In wet blasting, a slurry of water and fine abrasive is accelerated by compressed air to remove grinding residue, smooth weak edge defects, and create a controlled micro-texture before PVD or CVD deposition. For carbide inserts, drills, and end mills, that usually means better coating adhesion, fewer random edge failures, and more repeatable performance from batch to batch.
| Core Factor | Typical Conclusion |
|---|---|
| Process type | Wet blasting / slurry blasting pretreatment |
| Pressure range | Typically low-to-medium pressure for precision edge and surface conditioning |
| Main objective | Clean substrate, controlled edge state, and stable coating support |
| Dust condition | Low airborne dust compared with dry blasting |
| Typical workpieces | Carbide inserts, drills, end mills, reamers, wear parts |
| Typical supply pattern | Standard batch cabinets are usually faster to deliver than custom automated cells |
What Is cutting tool pretreatment before coating
Cutting tool pretreatment before coating is the controlled surface-preparation stage performed after grinding and before coating deposition. Its role is to remove contamination, stabilize the edge, and create a consistent surface condition so the coating is deposited onto a reliable substrate rather than onto residual swarf, oil films, oxide traces, or fragile micro-burrs left by previous operations.
In the broader family of industrial surface treatment, this process belongs to wet blasting, slurry blasting, and fine abrasive conditioning. Instead of using dry media alone, the system suspends abrasive particles in water and directs the slurry onto the tool surface with compressed air. That working principle is related to abrasive blasting methods, but the intent here is narrower and more technical: it is not just cleaning, but preparation of the cutting edge and tool faces for a later coating step.
Why Cutting Tool Pretreatment Before Coating Matters
A coating does not correct a weak substrate. If the underlying carbide or steel surface contains smeared material, loose debris, sharp micro-notches, or irregular edge remnants from grinding, the deposited layer can inherit those defects. Later, that may appear as coating peel-off, local chipping, inconsistent wear patterns, or unstable performance between tools that should be identical.
That is why coating pretreatment is best understood as a process bridge. It connects the grinding stage to the coating stage by reducing surface variability before the tool enters the deposition chamber.
Wet Blasting Within the Pretreatment Process Family
In cutting tools, pretreatment often overlaps with edge preparation. The same wet blasting cycle can clean the substrate, remove fragile burrs, and apply a measured edge hone that supports coating adhesion and edge strength. When the process is controlled correctly, it becomes possible to target a defined K-factor or edge radius rather than relying on uncontrolled manual touch-up.
That overlap is one reason tool manufacturers often evaluate edge honing of cutting tools together with coating pretreatment, especially for carbide inserts and solid-carbide rotary tools where pre-coating edge integrity is directly linked to field performance.
Core Selling Points of Wet Blasting Surface Treatment
The main benefits of wet blasting in this application are process cleanliness, controlled surface action, and repeatability. Water suppresses dust, cushions abrasive impact, and lowers the chance of harsh, uneven surface attack. On many precision tools, that makes it easier to produce a fine and uniform matte surface before coating.
A second benefit is lower risk of uncontrolled media impregnation on sensitive surfaces. A third is better repeatability when slurry concentration, nozzle condition, pressure, and fixture position are kept inside a defined process window. For plants focused on measurable process stability, wet blasting pretreatment is typically easier to standardize than hand finishing or loosely controlled dry blasting.
What This Step Is Not
Cutting tool pretreatment before coating is not bulk material removal, and it is not a substitute for correct grinding geometry. If the edge form, flute geometry, or chipbreaker profile is out of tolerance, wet blasting cannot reverse that. Its proper role is refinement and stabilization: cleaning, micro-texturing, and controlled edge conditioning of a tool that is already geometrically correct.
In practical production terms, the best results come when grinding quality, pretreatment, and coating are treated as one connected process chain rather than as isolated departments.
How Does cutting tool pretreatment before coating Work
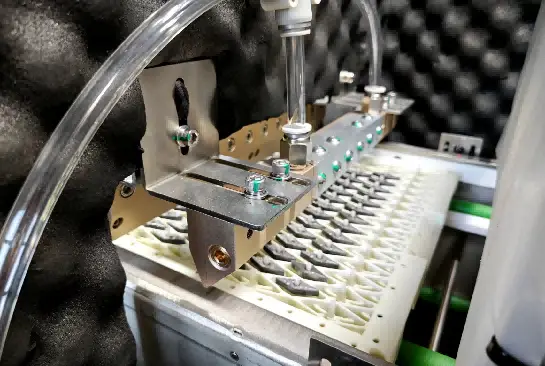
Cutting tool pretreatment before coating works by directing a regulated stream of water-borne abrasive particles onto the tool surface and edge zone. The slurry removes residual contamination and modifies the topmost surface layer through many fine impacts rather than through a heavy cutting action. Because the process energy can be tightly controlled, it is suitable for delicate substrate preparation on carbide inserts, drills, end mills, and similar tools.
Slurry System: Water Plus Abrasive Suspension
The process begins in a mixing and circulation tank, where water and abrasive are combined into a stable slurry. The abrasive must remain evenly suspended so that the process does not become stronger at the beginning of a cycle and weaker at the end, or vice versa. In precision pretreatment, consistency of slurry concentration matters as much as nominal pressure because both variables affect the removal rate and the resulting edge response.
Fine abrasive grades are typically preferred for coating-related work because they permit gentler, more uniform surface conditioning. Coarser media can increase aggressiveness, but they also widen the process window and can make very small edge targets harder to hold consistently.
Compressed Air Acceleration Path
Once the slurry is mixed, compressed air accelerates it through hoses and a nozzle toward the workpiece. The blast pattern is governed by nozzle diameter, stand-off distance, impact angle, dwell time, and traverse path. Each of those parameters changes how much energy reaches the rake face, flank face, chipbreaker, or edge line.
For example, a lower-angle approach may emphasize face cleaning and milder edge interaction, while a more direct angle can intensify local action. That is why pretreatment recipes must be matched to both tool geometry and the coating objective rather than copied blindly between products.
Fixture Design and Workpiece Orientation
The same blasting recipe can behave differently if workpiece presentation changes. Tool orientation, nest repeatability, spacing between parts, and shadowing effects all influence the final result. In insert production, fixture design is often the difference between a process that is nominally correct and one that is production-stable.
When rotary tools are involved, indexed rotation or servo-guided motion may be needed so the cutting edges see the same treatment around the circumference. That is particularly important where multiple flutes, unequal helix features, or asymmetric geometries are present.
Closed-Loop Slurry Recovery and Sedimentation
After impact, the used slurry drains back to the recovery circuit. There it carries worn abrasive, removed fines, carbide particles, and contamination from the workpiece surface. If those by-products are not managed, the slurry gradually becomes less predictable and the process window drifts.
Closed-loop recovery therefore does more than reduce consumable loss. It also supports process stability by returning slurry to a known operating condition. Sedimentation systems and controlled waste discharge remove accumulated sludge and degraded media so the effective cutting action remains more consistent through longer production runs.
Mist Control and Chamber Environment
Wet blasting reduces airborne dust, but it still creates water mist inside the enclosure. Effective mist extraction, chamber sealing, and viewing-window management are necessary for operator visibility, cleanliness, and routine maintenance. These features matter in production because unstable visibility often leads to inconsistent inspection and slower changeovers.
Where manual loading is used, the chamber environment also affects ergonomics and routine cleaning frequency. In short, reduced dust does not mean zero support requirements; it means the support systems are different.
Pressure Stability and Control Logic
For pretreatment work, the goal is rarely maximum pressure. What matters is a stable pressure band that delivers the same intensity day after day. Systems with pressure feedback and recipe management are better suited to this task because they reduce drift caused by air-supply fluctuation, nozzle wear, or operator adjustment.
This is where PID closed-loop pressure control becomes valuable. By holding pressure in a narrow band and pairing it with stored process recipes, the system helps maintain reproducibility across shifts and product families.
In pre-coating tool preparation, the most useful process is usually the one that removes variability, not the one that removes the most material.
| Process Parameter | Typical Range or Practice | Why It Matters |
|---|---|---|
| Working pressure | Typically about 0.15-0.45 MPa for precision pretreatment | Controls cleaning intensity and edge interaction |
| Slurry concentration | Commonly maintained in a controlled low-to-medium solids band, often set by validated recipe | Affects removal rate, finish consistency, and edge response |
| Abrasive particle size | Fine grades are usually preferred for coating pretreatment | Influences texture, edge rounding behavior, and surface uniformity |
| Nozzle stand-off and angle | Set by fixture design and part geometry; usually tightly controlled | Determines energy distribution across faces and cutting edge |
| Air flow and nozzle wear state | Checked as part of preventive maintenance | Affects actual impact energy even if pressure setting is unchanged |
| Media consumption and sludge load | Varies with abrasive breakdown, contamination, and discharge frequency | Influences both operating cost and process consistency |
| Control system | PLC/HMI recipe control with pressure feedback is typical in production systems | Supports repeatability, traceability, and shift-to-shift stability |
cutting tool pretreatment before coating vs Dry Blasting vs Other Methods
Cutting tool pretreatment before coating is often evaluated against dry blasting, shot peening, brushing, drag finishing, and vibratory finishing. All of those methods change a surface, but they do not create the same substrate condition or the same level of control at the cutting edge. The right choice depends on whether the plant prioritizes low dust, fine edge conditioning, broad smoothing, residual-stress effects, or the simplest possible equipment setup.
Wet Blasting vs Dry Blasting for Precision Tools
Wet blasting is usually selected when the coating process requires a clean, even, and reproducible substrate. The water phase suppresses dust and cushions particle impact, which can make the resulting finish finer and more uniform than with an equivalent dry process. That is especially relevant for carbide tools, where over-aggressive edge attack can weaken the very zone the coating is supposed to protect.
Dry blasting still has valid uses in heavy cleaning and rougher surface treatment. However, for pre-coating work on precision cutting tools, it can be harder to balance environmental control, edge sensitivity, and finish uniformity in a narrow process window.
Shot Peening and Mass-Finishing Alternatives
Shot peening has a different process goal. It is primarily a fatigue-oriented surface treatment, and the general terminology around the method is reflected in shot peening process definitions. That makes it useful in many engineering applications, but not always a direct substitute for pre-coating substrate conditioning on precision tools.
Vibratory and drag finishing can be effective for general deburring and broad-edge smoothing, yet they tend to act on the entire part in a less directional way. For cutting tools with sensitive geometries, wet blasting often offers better local control over the edge zone and tool faces.
| Evaluation Dimension | Wet Blasting Pretreatment | Dry Blasting | Shot Peening | Vibratory / Drag Finishing |
|---|---|---|---|---|
| Main purpose | Surface cleaning, micro-texturing, and edge-zone conditioning | General blasting and rougher cleaning | Fatigue-oriented surface treatment | Whole-part smoothing and deburring |
| Dust generation | Low relative to dry blasting | High unless extraction is extensive | Moderate in enclosed systems | Low airborne dust, but media and compound handling are required |
| Surface finish control | Fine, even matte finish is typical | Rougher finish is more common | Functional peened texture | Broad smoothing effect |
| Media embedding risk | Lower on many sensitive surfaces due to water film | Higher on some substrates | Depends on media and substrate | Different mechanism; not directly comparable |
| Edge-zone repeatability | High with stable fixturing and recipe control | Moderate | Limited for precision edge shaping | Moderate, often less directional |
| Environmental handling | Slurry, mist, and sludge management | High dust-collection burden | Dry-media containment and recovery | Media, compound, and wastewater management |
| Typical fit for coated cutting tools | Strong fit for pre-coating conditioning | Selective fit | Indirect fit | Selective fit depending on geometry |
Key Specifications to Evaluate Before Buying
The first buying criterion is not machine size but process objective. A buyer should define the tool substrate, tool geometry, post-grinding condition, target edge state, planned coating type, and quality criteria for surface cleanliness before comparing equipment. Without that definition, even a well-built machine may be the wrong process platform.
Pressure Window and Repeatability
For cutting tool pretreatment before coating, the usable pressure band matters more than the maximum catalog pressure. A system that reaches very high values but cannot hold a stable low-to-medium operating range is usually less suitable than a machine that delivers steady pressure with minimal drift. Repeatability is what protects coating consistency.
Pressure should be evaluated together with nozzle condition and air supply stability. A nominal setpoint has little meaning if actual blast energy changes because of wear or fluctuating plant air.
Motion Precision and Fixture Strategy
Motion capability is the next filter. Standard insert batches may be processed effectively in a fixed chamber with repeatable nests, while drills, taps, end mills, and special forms often benefit from indexed presentation or servo-linked nozzle motion. In those cases, servo X/Y/Z accuracy becomes part of the process specification rather than just an automation feature.
Fixture design should be reviewed at the same time. The machine can only be as repeatable as the workholding that presents the tool to the blast zone.
Throughput, Changeover, and Recipe Control
Throughput should be measured using the full cycle: load, blast, rinse if applicable, unload, inspect, and recover to the next stable batch. Plants that run many tool families often discover that changeover discipline matters as much as nominal cycle speed.
Recipe management is critical in that environment. HMI-based programs, alarm logs, permission levels, and validated parameter storage reduce the chance that operators will improvise settings between shifts or product runs.
Footprint, Utilities, and Maintenance Access
Wet blasting systems require more than floor space. Buyers should confirm compressed air demand, electrical supply, water management, drainage, mist extraction, maintenance clearance, and sludge disposal routines before final layout approval. A compact machine can still be impractical if daily maintenance is difficult or if utility routing is poor.
Waste Handling and Safety Features
Sludge management is a process-control issue as well as a housekeeping issue. If worn media and fines remain in circulation too long, process intensity changes. Systems with automatic waste-sand sedimentation help narrow that variability while reducing manual cleanup burden.
Safety review should include interlocks, emergency stops, sealed access points, visibility, operator posture, and maintenance procedures. For exported equipment, buyers may also want to map the machine against their site-specific compliance requirements and the broader surface preparation standards framework.
Applications Across Industries
Although the target keyword is cutting tool pretreatment before coating, the same wet blasting principles apply across a wide range of industrial finishing tasks. Once abrasive grade, nozzle geometry, fixture style, and motion pattern are adjusted, the core process can serve everything from selective deburring to additive-manufacturing cleanup and cosmetic texturing.
In toolmaking, the most direct use case is pre-coating edge and surface conditioning. In adjacent industries, the same equipment class may be used for deburring, descaling, paint-line pretreatment, and surface refinement of difficult geometries. That wider relevance is one reason wet blasting is often adopted as a process platform rather than as a single-purpose machine.
A facility that already handles machined components in addition to cutting tools may also use the same process family for burr removing of metal parts or for broader coating pretreatment wet blasting applications where a controlled substrate is required before painting, plating, or conversion treatment.
| Application Type | Target Industry | Workpiece Example | Process Benefit |
|---|---|---|---|
| Edge and pre-coating conditioning of cutting tools | Carbide tool manufacturing | Inserts, drills, end mills, reamers | Clean substrate and more stable coating support |
| Burr removal | Precision metal parts | Stamped parts, machined components, sintered parts | Selective deburring with controlled surface impact |
| Scale removal | Steel and forging production | Bars, forgings, heat-treated parts | Oxide removal before downstream machining or finishing |
| Pretreatment before coating | Industrial finishing and fabrication | Metal parts before paint or conversion coating | More consistent surface cleanliness and adhesion support |
| AM post-processing | Additive manufacturing | 3D-printed metal components | Surface refinement and loose-powder cleanup |
| Peening of metal parts | Mechanical component production | Fatigue-sensitive metal parts | Functional surface conditioning |
| Glass frosting | Architectural and specialty glass | Decorative or technical glass panels | Uniform matte appearance |
| 3C device finishing | Consumer electronics supply chain | Frames, housings, device covers | Fine smoothing and cosmetic consistency |
Equipment Selection Guide
Selecting equipment for cutting tool pretreatment before coating starts with production scale and geometric complexity. R&D labs usually need flexibility to test abrasive grades, nozzle angles, and edge targets, while mature production cells need repeatability, locked recipes, and predictable throughput.
R&D and Process Validation
At the development stage, flexible sample testing often matters more than hourly output. A robot-type R&D blasting cell is typically suited to this phase because it supports variable tool presentation, recipe trials, and process verification across small batches and mixed geometries.
Standard Batch Production
Once the process window is established, standard batch equipment often becomes the most practical choice. For many carbide insert and small-tool programs, a single-chamber batch cabinet offers a stable balance of throughput, fixture repeatability, and manageable changeover. If output demand rises, the next step is often higher utilization rather than a complete change in process principle.
Matching Configuration to Application
The selection matrix below summarizes eight common equipment formats that can support cutting tool pretreatment before coating or closely related wet blasting applications. It is intended as a process guide, not as a fixed specification sheet, because tool geometry, fixture logic, and abrasive choice still determine the final process capability.
| Configuration / Model Tier | Target Production Scale | Workpiece Size Range | Precision Level | Recommended Applications |
|---|---|---|---|---|
| 1. Bench development unit | Lab feasibility and abrasive screening | Small tools and coupons | Moderate | Early process proofing |
| 2. Flexible R&D robot cell | Pilot validation and sample testing | Small precision tools | High | Mixed geometries and angle trials |
| 3. Manual flexible cabinet | Small-batch, high-mix production | Small tools and special parts | Moderate | Frequent changeovers |
| 4. Standard single-chamber batch system | Routine batch production | Small to medium tool families | High | Stable recipe-based pretreatment |
| 5. Single-piece process machine | Medium-volume discrete flow | Individual high-value tools | High | Tight traceability and cycle control |
| 6. Servo multi-axis precision cell | Advanced precision production | Complex tool geometries | Very high | Directional treatment of difficult surfaces |
| 7. Double-chamber utilization system | Higher-throughput batch output | Repetitive tool programs | High | Parallel loading and better utilization |
| 8. Custom integrated finishing line | Dedicated industrial workflow | Application-specific range | High to very high | In-line pretreatment before downstream finishing |
Cost, Lead Time and ROI Considerations
Machine price in this segment is driven more by process control and automation depth than by cabinet size alone. A simple wet blasting cabinet may be enough for general cleaning, but cutting tool pretreatment before coating often requires better pressure regulation, more repeatable fixturing, tighter motion control, stronger recipe discipline, and more robust slurry management. Those elements increase capital cost, yet they also determine whether the process can hold narrow quality limits.
Lead time usually scales with customization. A standard batch platform can often be supplied on a shorter schedule than a servo-driven precision cell, a single-piece automated system, or an integrated line that requires sample verification and fixture development. For that reason, lead times are best treated as typical bands rather than hard promises until the process route is frozen.
ROI should be assessed in layers rather than by a single machine-hour calculation. The first layer is labor reduction and process formalization: replacing manual cleaning, manual edge touch-up, or inconsistent hand finishing with a defined and repeatable method. The second layer is reduced rework, because tools entering the coating stage with a more stable substrate condition are less likely to show preventable adhesion or edge-related failures.
The third layer is performance consistency in use. A properly tuned pretreatment process often works together with edge preparation to reduce random early failure and support the coating at the cutting edge. That can contribute to tool life uplift and, just as important, to tighter performance spread across production lots.
The fourth layer is scrap and troubleshooting efficiency. When grinding quality, pretreatment quality, and coating quality are separated into measured steps, the manufacturer can diagnose root causes more quickly. In high-value carbide production, that process visibility can be economically significant even if it does not appear directly in a simple payback formula.
Operating cost should also be reviewed realistically. Abrasive replenishment, nozzle wear, pump components, mist extraction upkeep, sludge handling, and preventive maintenance all affect the true cost per tool or per batch. A lower entry price is not automatically a lower cost of ownership if the machine is difficult to keep stable in daily production.
Why Choose DassiAuto — Our Company
DassiAuto Intelligent Equipment Co., Ltd is a Chinese manufacturer established in 2012 and focused on wet blasting technology for industrial surface treatment. Based on the company context provided for this article and summarized in about DassiAuto, the company operates as a national high-tech enterprise under the ISO 9001 quality management standard and holds invention patents, utility model patents, and software copyrights covering blasting equipment and control systems. Its wet blasting range includes eight equipment configurations for R&D, batch production, and application-specific use, with engineering features that include PID closed-loop slurry pressure control, servo-driven X/Y/Z linkage with 0.02 mm control accuracy, HMI recipe management with hierarchical permission control, automatic waste-sand sedimentation with one-click discharge, and dust-collection systems that reduce water mist. The same source context identifies customer references including Wecan Cutting Tools, Ruian Carbide Tools, Huareal, Metcera, OKE, YG, Kelite, and XTC, and describes a service model covering sample testing, planning, design, manufacturing, installation, commissioning, training, after-sales support, spare parts, abrasive resupply, and process optimization.
FAQ
Q1. Is sample testing necessary for cutting tool pretreatment before coating?
In most cases, yes. Sample testing verifies whether the selected abrasive, pressure window, fixture design, and cycle time can produce the required substrate condition and edge state before the process is released for production.
Q2. Can one wet blasting machine handle inserts, drills, and end mills on the same platform?
It can, but only if the platform has suitable fixtures, recipe management, and enough flexibility in nozzle orientation or motion control. Mixed-tool production is common, yet repeatability depends on presenting each geometry to the blast stream in a controlled and repeatable way.
Q3. What information should a buyer prepare before requesting a quotation?
The most useful inputs are tool drawings, substrate grade, post-grinding condition, target edge specification, planned coating route, expected output, and known failure modes such as weak adhesion or early chipping. Those details help determine whether the project fits a standard cabinet, a flexible R&D cell, or a more specialized precision configuration.
Q4. How long does installation and commissioning usually take?
The timeline depends on how standardized the machine is and how much application development remains. A routine batch cabinet is usually faster to install and qualify than a customized servo-driven system that requires fixture tuning and recipe validation on several tool families.
Q5. What consumables and spare parts matter most in this process?
The main recurring items are abrasive media, nozzles, hoses, seals, pump wear parts, cabinet protection components, and sludge-management parts. In precision pretreatment, the consumables that affect blast pattern, slurry condition, and pressure stability deserve the closest monitoring.
Q6. How should after-sales support be evaluated for a coating-pretreatment project?
After-sales support should be judged by process continuity, not only by repair response. The most useful support typically includes spare-parts planning, abrasive resupply, operator retraining when tool families change, and assistance with revalidating recipes after changes in grinding condition, substrate, or coating process.