Quick Answer
For precision parts, liquid honing is often a better choice than dry blasting when the priority is a controlled finish, lower airborne dust, and gentler surface action. The process uses water, fine abrasive media, and compressed air to create a slurry stream that cleans, deburrs, textures, or edge-prepares the workpiece with high consistency. In industrial production, it is widely used for carbide tools, machined metal parts, additive-manufactured components, glass, and visible consumer-product surfaces where repeatability matters more than the fastest possible cut rate.
| Core factor | Typical conclusion |
|---|---|
| Process type | Wet blasting process using water-borne abrasive slurry |
| Pressure profile | Typically low to medium, adjusted by material, geometry, and finish target |
| Surface effect | Uniform matte, satin, or refined technical finish |
| Dust behavior | Significantly reduced free airborne dust compared with dry blasting |
| Common applications | Edge honing, selective deburring, coating pretreatment, AM finishing, glass frosting |
| Delivery profile | Typical lead time is shorter for standard cabinets and longer for custom automation |
What Is liquid honing
Liquid honing is a precision surface-treatment process in which abrasive particles are suspended in water and then accelerated onto a workpiece by compressed air. In many factories, the term is used interchangeably with slurry blasting, wet blasting, vapor blasting, or wet sandblasting, although “liquid honing” usually implies a finer, more controlled finishing objective rather than aggressive stripping.
Technically, liquid honing belongs to the wet blasting family of abrasive processes. The water phase does not replace the abrasive; it carries and cushions the media. That distinction is important, because the process remains a true abrasive treatment, capable of cleaning, edge radiusing, texturing, descaling, deburring, and cosmetic finishing depending on media choice, pressure, nozzle path, and stand-off distance.
Compared with dry blasting, liquid honing changes the impact behavior at the surface. The water film suppresses much of the dust that would otherwise be generated, helps flush away broken fines and detached contamination, and moderates particle impact. In practice, that can reduce harsh surface attack and make the resulting finish more uniform, especially on precision-machined parts, coated substrates, sharp-edge features, and complex geometries.
The process is widely chosen where the surface result must be both functional and visually consistent. Examples include carbide cutting tools that need controlled edge preparation, machined housings requiring burr removal without excessive roughness, forged parts needing scale removal before inspection, and decorative or consumer-facing parts where a consistent satin texture is required.
Liquid honing also fits well into modern process-control thinking. Once media type, slurry concentration, pressure, nozzle geometry, and cycle time are validated, the process can be repeated with relatively low operator variation. That is why it is common in technical finishing cells rather than only in general cleaning departments.
From an industrial buyer’s point of view, the core selling points are clear: lower dust burden, lower risk of media embedding on sensitive surfaces, more even texture, and tighter process repeatability than many manually operated dry-blast routines. Those advantages explain why liquid honing is regularly evaluated for higher-value parts where rework or surface inconsistency is costly.
How Does liquid honing Work
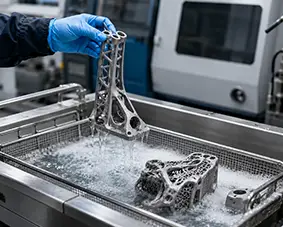
Liquid honing works by circulating a mixture of water and abrasive through a sealed blasting system, then using compressed air to project that slurry through one or more nozzles toward the workpiece. Although the concept is straightforward, reliable industrial performance depends on how well the machine controls slurry condition, pressure stability, recirculation, mist management, and part handling during continuous operation.
Slurry preparation and media suspension
The process begins in a slurry tank where water and abrasive are mixed to a defined concentration. The concentration has to stay within a practical operating window, because too little abrasive lowers processing efficiency while too much can destabilize flow and accelerate wear. Agitation or circulation keeps the media suspended so the slurry delivered to the nozzle remains consistent from the first part to the last.
Media selection determines much of the final result. Fine grades are commonly used for cosmetic refinement, edge preparation, and uniform matte finishes. Coarser or harder media may be selected for more assertive deburring, scale removal, or surface activation before a downstream coating step.
Compressed-air acceleration and nozzle impact
At the gun or nozzle, compressed air accelerates the slurry toward the target surface. The energy at impact is influenced by pressure, nozzle diameter, stand-off distance, attack angle, traverse speed, and the abrasive particle-size distribution. That combination decides whether the process behaves like gentle cosmetic finishing or like a stronger technical deburring treatment.
Because abrasive grains are carried in water, the impact is cushioned relative to dry blasting. The abrasive still cuts or peens the surface, but usually with less violent local attack. That moderated behavior is one reason liquid honing is favored for parts with tight dimensional expectations or finish-sensitive visible zones.
Closed-loop recovery and sediment handling
After impact, the slurry drains back into the recovery section of the machine. Reusable water and abrasive are recirculated, while contaminants such as removed burr fragments, oxide fines, sludge, and worn media are separated out through sedimentation and discharge mechanisms. Good recovery design is essential to maintain quality, because contaminated slurry behaves differently even if the nominal pressure setting has not changed.
In production, waste handling is not a minor housekeeping issue. If sludge accumulates or spent fines remain in circulation too long, cut rate, finish appearance, and recipe stability can drift. Machines with automatic sedimentation and one-click waste discharge therefore have a practical advantage in maintaining consistent output over long runs.
Mist extraction and chamber visibility
Liquid honing produces far less free dust than dry blasting, but it still creates water mist inside the enclosure. That mist must be controlled to preserve operator visibility, protect internal components, and keep the working environment cleaner. Industrial systems typically include extraction and mist-management hardware rather than relying on enclosure sealing alone.
Pressure stability and digital control
For precision applications, absolute maximum pressure matters less than stable pressure over time. PID-based regulation helps keep slurry delivery steady as hoses age, media conditions shift, or cycle demand changes. This is especially valuable where edge radius, cosmetic appearance, or coating pretreatment consistency must stay inside a narrow process window.
Recipe-based control is equally important. Once an acceptable parameter set is proven, storing that recipe in the HMI reduces operator-to-operator variation and speeds changeovers between different part families. That is one reason many modern users see closed-loop slurry control and recipe management as quality tools, not just convenience features.
In liquid honing, repeatable results come from controlling slurry quality, pressure, motion, and recovery as a single integrated system.
| Parameter | Typical industrial practice | Why it matters |
|---|---|---|
| Working pressure | Typically set in a low-to-medium range according to material and finish target | Controls impact energy and removal intensity |
| Slurry concentration | Usually maintained within a validated weight or volume window | Affects cut rate, coverage density, and finish consistency |
| Abrasive particle size | Fine to medium particle ranges are common for precision work | Influences roughness, edge rounding, and visual texture |
| Air flow demand | Depends on nozzle size, pressure, and number of blast guns | Determines utility sizing and delivery stability |
| Media consumption rate | Varies by abrasive durability, contamination load, and cycle severity | Drives consumable cost and process drift risk |
| Stand-off distance | Normally fixed by recipe, fixture, or programmed motion path | Changes local coverage and uniformity |
| Control system | Manual adjustment or PLC/HMI recipe management | Supports repeatable setup and reduced operator variation |
| Recovery method | Closed-loop recirculation with sedimentation and mist extraction | Maintains slurry quality and cleaner operation |
liquid honing vs Dry Blasting vs Other Methods
Liquid honing is most frequently compared with dry blasting because both are nozzle-based abrasive processes, yet they behave differently in the blast zone and in the plant environment. Dry blasting is often preferred for aggressive cleaning, fast rust removal, or creating a rough anchor profile. Liquid honing is more commonly selected when the surface change must be controlled and when dust burden or finish refinement is a major concern.
It is also useful to compare liquid honing with adjacent finishing methods. Shot peening can use related hardware, but its main objective is controlled compressive stress and fatigue performance rather than general cleaning or cosmetic finishing, as reflected in shot peening process terminology. Vibratory finishing, by contrast, is excellent for bulk smoothing of many small parts, but it cannot always match the local targeting and geometry-specific control available from a nozzle-driven wet process.
| Evaluation factor | Liquid honing | Dry blasting | Shot peening | Vibratory finishing |
|---|---|---|---|---|
| Primary purpose | Controlled cleaning, deburring, texturing, edge prep, cosmetic finishing | Fast stripping, descaling, roughening, general cleaning | Surface stress conditioning and fatigue-related treatment | Batch smoothing, edge softening, and mass finishing |
| Airborne dust | Low free dust due to water phase | High unless strongly enclosed and extracted | Process-dependent, usually less about dust than intensity control | Low airborne dust, but compound and media management remain |
| Surface character | Fine, even, matte or satin finish | More aggressive and often rougher | Functional peened texture | Broadly smoothed over longer cycles |
| Media embedding risk | Lower on many sensitive or softer surfaces | Higher on some soft or coated substrates | Depends on media and specification | Generally low projected-impact risk |
| Local selectivity | High with nozzle path and fixture control | High, but with heavier dust-management burden | Moderate to high in dedicated peening cells | Lower, because parts are processed more generally |
| Process repeatability | High with stable slurry and pressure control | Can drift with feed variation and manual setup changes | High when intensity and coverage are qualified | Good for batch lots, less precise on local zones |
| Environmental handling | Wet waste and sludge management | Dust collection and dry-media housekeeping | Specification-driven process control | Media wear and liquid-compound disposal management |
In coating-related work, liquid honing may also align well with surface preparation practices from AMPP because the process combines mechanical cleaning with a comparatively controlled operating environment. That does not make it automatically superior in every case, but it explains why engineers evaluate it when they want consistent pretreatment on precision or visible parts rather than only maximum stripping speed.
Key Specifications to Evaluate Before Buying
A liquid honing machine should be specified from the required process result backward, not from the brochure headline forward. Buyers need to decide whether the real objective is edge honing, selective deburring, oxide removal, cosmetic texturing, frosting, peening, or pretreatment before painting or coating. Each of those tasks imposes different demands on pressure stability, media control, nozzle motion, and part handling.
Pressure window and delivery stability
Pressure range matters, but stable delivery matters more. A machine that can hold a validated pressure band through long shifts will usually outperform a machine that advertises only a higher maximum number. Consistent delivery supports predictable roughness, edge radius, burr-removal threshold, and visual appearance.
Slurry system design and media compatibility
The slurry circuit should maintain suspension, minimize dead zones, and allow practical removal of fines and contamination. Buyers should ask how the system handles settling, recirculation, sludge discharge, and media replenishment. The machine also needs to be compatible with the abrasive grades required for the intended substrates and finish classes.
Motion control and nozzle positioning accuracy
Where the process depends on precise attack angle and stand-off distance, servo motion becomes a central specification. According to the supplied company context, DassiAuto’s wet blasting equipment includes servo-driven X/Y/Z linkage with 0.02 mm accuracy, which is particularly relevant for controlled edge preparation, narrow tolerance windows, and multi-face parts with complex geometry.
Throughput, cycle time, and loading logic
Actual output should be measured in qualified parts per shift rather than nominal blast minutes. Part loading, fixturing, draining, recipe recall, unloading, and inspection all affect throughput. For many plants, changeover time and ergonomic loading design have as much impact on productivity as nozzle power.
Chamber workspace and plant footprint
The useful internal workspace is more important than external machine dimensions alone. Buyers should verify part clearance, fixture envelope, maintenance access, and the routing of utilities, drainage, and extraction. Plate parts, long bars, and awkward three-dimensional components often require application-specific machine geometry rather than a standard cabinet.
HMI, recipe management, and permission control
Recipe storage is essential where multiple part families share one machine. HMI control with user permissions helps protect validated settings and reduces the risk of uncontrolled trial-and-error changes on the shop floor. For technical finishing cells, that contributes directly to scrap reduction and traceable process discipline.
Mist extraction, waste-sand handling, and safety
Even though liquid honing suppresses dust, it still generates mist, sludge, and spent abrasive fines. Buyers should examine extraction performance, chamber visibility, sediment discharge, access for cleaning, interlocks, emergency stops, and utility safeguards. Those features affect daily usability, uptime, and maintenance labor just as much as they affect compliance.
Applications Across Industries
Liquid honing serves a wide spread of industries because it can be tuned for both functional and cosmetic outcomes. The same process family can prepare a cutting-tool edge before coating, remove burrs from a stainless machined part, clean forge scale from a bar product, or create a consistent matte finish on a visible consumer-device housing. What unites these applications is the need for controlled surface modification rather than uncontrolled aggression.
Toolmaking is one of the clearest examples. Manufacturers using edge honing of cutting tools often rely on liquid honing when they need repeatable K-factor control, uniform edge preparation, and a finish suitable for later coating. In general metalworking, burr removal processing is a natural fit because the slurry stream can remove fragile burrs while preserving the broader surface more evenly than many manual dry methods.
Pretreatment is another major category. Parts destined for paint or conversion layers may benefit from coating pretreatment wet blasting when the objective is uniform cleanliness and a controlled surface state before downstream finishing. Other sectors use liquid honing for additive-manufactured metal parts, functional peening, glass frosting, and cosmetic refinement of 3C products where tactile feel and visible uniformity matter.
| Application type | Target industry | Typical workpiece | Process benefit delivered |
|---|---|---|---|
| Edge honing of cutting tools | Carbide tool manufacturing | Inserts, drills, end mills | Controlled edge preparation and coating readiness |
| Burr removing of metal parts | Precision machining, automotive supply, general metalworking | Valve bodies, brackets, housings | Selective deburring with repeatable surface quality |
| Scale removal from forgings | Forging and steel processing | Bars, shafts, forged blanks | Cleaner surface for inspection and later finishing |
| Pretreatment before coating | Fabrication, appliance, coatings supply chains | Steel and aluminum components | More uniform cleanliness and adhesion consistency |
| Post-processing of AM parts | Additive manufacturing | Metal 3D-printed functional parts | Removal of adhered particles and improved appearance |
| Peening of metal parts | Automotive and industrial mechanical components | Loaded metallic parts | Functional conditioning of the outer surface |
| Glass frosting | Glass processing and display products | Panels, covers, decorative glass | Even matte texture and visual consistency |
| 3C device finishing | Consumer electronics | Frames, housings, covers, shells | Controlled cosmetic smoothness and tactile finish |
Equipment Selection Guide
Selecting liquid honing equipment requires matching the machine architecture to the real production pattern. Some users need flexibility for sample development and frequent recipe changes. Others need stable throughput on one part family, where chamber utilization, fixture repeatability, and service access become more important than broad versatility.
A useful approach is to compare equipment by configuration tier rather than by a single headline spec. In practice, liquid honing systems range from development-oriented cells through standard batch cabinets and into application-specific machines for flat parts, round rods, or complex multi-axis components. The right choice depends on whether the plant values precision, throughput, geometry reach, or rapid validation.
| Configuration or model tier | Target production scale | Workpiece size range | Precision level | Recommended applications |
|---|---|---|---|---|
| R&D lab-scale flexible cell | Sample testing and process development | Small to medium mixed parts | High | Feasibility studies, process development, short-run precision finishing |
| Standard manual cabinet | Low-volume technical processing | Small parts | Medium | Repairs, pilot work, custom finishing |
| Single-chamber batch cabinet | Routine batch manufacturing | Small to medium parts | Medium to high | Repetitive deburring, edge prep, cosmetic processing |
| Single-piece dedicated machine | Stable one-piece flow | Small to medium individual parts | High | Fixed part families requiring cycle consistency |
| Double-chamber production system | Higher-throughput repetitive work | Small to medium parts | Medium | Alternating load-and-blast sequences |
| Servo multi-axis complex-part system | Precision treatment of intricate geometry | Complex 3D components | High | Multi-face parts and geometry-sensitive zones |
| Plate-part large-workspace machine | Broad-surface processing | Flat or plate-shaped parts | Medium | Panels, plates, and uniform texturing |
| Round-rod continuous system | Long-product processing | Rods, shafts, bar stock | Medium | Descaling and conditioning of cylindrical workpieces |
For sample validation and flexible process development, the RB-6 R&D wet blasting cell suits mixed-part programs where frequent trials are expected. For routine batch production, a single-chamber batch cabinet is more appropriate when the goal is repeatable day-to-day processing. Where throughput is the main driver, a double-chamber production system can support alternating loading and blasting logic with less idle time between cycles.
Cost, Lead Time and ROI Considerations
The cost of a liquid honing system depends far more on configuration depth than on the process name alone. A basic cabinet with manual controls and simple recovery hardware has a very different cost structure from a servo-driven, recipe-controlled cell with custom fixtures, advanced mist extraction, and automated sludge handling. For this reason, buyers should focus on total cost per qualified part rather than only on initial machine price.
Automation is often the biggest capital-cost driver. Servo axes, PLC logic, HMI recipe storage, permission control, special nozzles, and custom part handling all add engineering content. Chamber size, wear-liner specification, pump selection, recovery design, and extraction performance also affect cost because they influence both manufacturing scope and long-term maintenance exposure.
Lead time should be discussed as typical, not absolute. Standard machines generally move faster through design and build than highly customized cells for one geometry family or an integrated pretreatment line. Process approval, fixture validation, and sample testing can add time, especially when the acceptance criterion is not only roughness but also edge profile, cosmetic appearance, or downstream coating performance.
ROI usually comes from a combination of labor reduction, improved quality stability, and lower downstream loss. In deburring, liquid honing can reduce hand-finishing hours and improve consistency. In edge preparation, it can support more repeatable tool-edge condition before coating. In pretreatment, it can stabilize surface cleanliness and reduce the probability of later coating or bonding defects.
The strongest returns often appear where part value is high and rework is expensive. If a factory is losing margin to cosmetic rejects, burr-related assembly problems, unstable surface finish, or inconsistent edge preparation, liquid honing may justify itself even when it is not the most aggressive material-removal method. That logic aligns with broader manufacturing process control guidance from NIST, which emphasizes repeatability, validation, measurement discipline, and reduced variation as drivers of manufacturing efficiency.
Why Choose DassiAuto — Our Company
DassiAuto Intelligent Equipment Co., Ltd is a Chinese manufacturer established in 2012 and focused on wet blasting technology for industrial surface treatment. Based on the supplied company context and the company background page, it is a national high-tech enterprise operating under the ISO 9001 quality management standard, with invention patents, utility model patents, and software copyrights covering blasting equipment and control systems. The company states that it covers planning, design, manufacturing, sales, and application development across the surface-treatment equipment value chain. Its lineup includes eight wet blasting equipment configurations serving R&D, batch production, and application-specific processing, with engineering features such as PID closed-loop slurry pressure control, servo-driven X/Y/Z linkage to 0.02 mm accuracy, HMI recipe management with hierarchical permission control, automatic waste-sand sedimentation with one-click discharge, and dust-collection systems that reduce water mist. The supplied context also lists customer references including Wecan Cutting Tools, Ruian Carbide Tools, Huareal, Metcera, OKE, YG, Kelite, and XTC. Its full-cycle service model runs from application development and sample testing through planning, design, manufacturing, installation, commissioning, training, after-sales support, spare parts, TR-series abrasive supply, and process optimization.
FAQ
Q1. Is there a minimum order quantity for a liquid honing machine?
For capital equipment, procurement is usually handled as a project purchase rather than as a conventional MOQ item. The practical minimum is normally one machine, but configuration depth, fixtures, and process-development scope will vary according to the application.
Q2. Should buyers send parts for trial processing before placing an order?
Yes, in most cases trial processing is advisable. It helps confirm media grade, pressure window, cycle time, achievable finish, and whether the process can meet both functional and cosmetic targets on the real substrate and geometry.
Q3. Can a liquid honing system be customized for one specific workpiece family?
Yes. Many industrial systems are configured around one part type, one loading method, or one geometry class to improve cycle stability and reduce changeover error. Customization typically covers nozzles, fixtures, motion paths, chamber dimensions, and recovery logic.
Q4. What is normally included in installation and commissioning?
Typical scope includes machine placement, utility connection guidance, startup checks, parameter verification, and trial production confirmation. For automated systems, commissioning may also cover recipe setup, interlock verification, and operator permissions.
Q5. How much operator training is usually required?
Training generally covers slurry preparation, recipe selection, nozzle wear inspection, sediment discharge, daily checks, and basic troubleshooting. More automated machines also require instruction on HMI navigation, alarm response, and how to preserve validated process settings.
Q6. What after-sales support matters most for long-term liquid honing stability?
The most important support areas are spare-parts availability, matched abrasive resupply, troubleshooting response, and continuing process optimization when results begin to drift. Stable long-term output depends on consistent consumables, disciplined maintenance, and technical support that can restore the validated process window quickly.