Quick Answer
For precision parts, wet blasting is often preferred when the goal is a cleaner process window, lower airborne dust, tighter finish consistency, and gentler abrasive action than conventional dry blasting. Because abrasive is carried in water as a slurry, the process can reduce dust, limit heat buildup, and produce a more uniform cosmetic or functional surface on carbide tools, metal parts, glass, and additively manufactured components. It is especially valuable where deburring, edge honing, coating pretreatment, or fine surface conditioning must be repeatable across batches.
| Core factor | Typical conclusion |
|---|---|
| Process type | Water-abrasive slurry accelerated by compressed air |
| Working pressure band | Typically low-to-medium blasting pressure, tuned to substrate and finish target |
| Surface result | Fine, even matte finish with controlled micro-erosion |
| Dust behavior | Strong dust suppression compared with dry blasting |
| Typical uses | Edge honing, deburring, coating pretreatment, AM post-processing, cosmetic finishing |
| Typical project timeline | Lead time varies by configuration, automation level, and validation scope |
What Is wet blasting
Wet blasting is an abrasive surface treatment process in which water and blasting media are mixed into a slurry and propelled onto a workpiece. In industry, the process is also called wet sandblasting, slurry blasting, or vapor blasting, although the exact equipment layout and pressure strategy can vary by manufacturer and application.
Within the broader abrasive blasting family, wet blasting sits between aggressive dry media projection and gentler finishing methods such as vibratory processing. It is used when manufacturers want cutting action from abrasive particles but also need better finish control, less airborne contamination, and less risk of over-processing delicate features.
The technical logic is straightforward. Water acts as the carrier phase, suspending abrasive particles and moderating impact behavior. That damped impact can make the process more suitable for fine deburring, edge preparation, oxide removal, and cosmetic texturing where the finish must look consistent and the substrate cannot tolerate excessive embedding or heat.
Three selling points explain why wet blasting has become important in precision manufacturing. First is dust suppression: the water phase captures much of the particulate that would otherwise become airborne in a dry process. Second is uniform surface finish: the slurry cushions particle impact enough to support more even material removal on many metals, carbides, ceramics, and glass. Third is process repeatability, especially when the machine maintains stable slurry concentration, nozzle motion, and pressure over time.
A related advantage is reduced risk of abrasive impregnation on softer or coated surfaces. In many applications, the water film helps separate particle impact from direct dry contact, which can reduce surface contamination compared with some dry blasting setups. That does not eliminate the need for process trials, but it does widen the usable process window for parts that need clean post-treatment results.
From a production perspective, wet blasting is not a single machine type. It can be configured as R&D equipment, batch cabinets, servo multi-axis systems, large-format machines for flat parts, systems for cylindrical bars, or integrated pretreatment lines. That range is one reason the process appears in toolmaking, metalworking, coating lines, glass finishing, and electronics enclosure production.
In practical manufacturing terms, wet blasting is best understood as a controllable abrasive finishing process rather than simply a dust-reduced version of dry blasting.
For terminology background, the broader abrasive blasting process family is commonly defined by media acceleration method, media type, and intended surface outcome. In coating and protection workflows, preparation quality is also tied to surface profile, cleanliness, and process control principles discussed by AMPP surface preparation guidance.
How Does wet blasting Work
Wet blasting works by circulating a slurry, accelerating it through a nozzle with compressed air, directing it at the target area, and then recovering the used slurry for recirculation or waste separation. The equipment may look simple from outside, but the process depends on stable fluid mechanics, controlled media concentration, and reliable recovery.
Slurry generation and suspension control
The first stage is slurry preparation. Water and abrasive are mixed in a tank or pressure vessel so that the abrasive remains suspended instead of settling immediately. Agitation, recirculation pumps, and tank geometry all matter here because inconsistent suspension leads directly to inconsistent surface finish.
In a properly tuned system, slurry concentration is selected according to substrate hardness, desired roughness, burr size, and required removal rate. A tool edge-honing application may need a different solids loading than forged-part cleaning or glass frosting. If concentration drifts, the same air pressure can produce very different cutting intensity.
Compressed air acceleration path
The second stage is acceleration. Compressed air introduces energy into the flow and drives the slurry through hoses and a nozzle toward the workpiece. Nozzle geometry, standoff distance, impingement angle, and traverse speed determine how much material is removed and how the finish develops across the part.
Compared with dry blasting, the presence of water changes the particle dynamics. Impact energy is still significant, but the water phase damps some of the sharp, ricocheting interaction seen in dry systems. That is one reason wet blasting can produce a more even, satin-like finish on many parts.
Workpiece handling and motion control
The third stage is part presentation. Basic systems rely on manual manipulation, while advanced systems use indexed fixtures, rotary axes, or servo-driven X/Y/Z motion to maintain nozzle position and angle. DassiAuto’s engineering context specifies 0.02 mm servo accuracy for X/Y/Z linkage, which is relevant when edge radius, localized deburring, or patterned blasting must be controlled across complex geometry.
Recipe-based HMI control matters here because process success depends on repeatable combinations of pressure, flow, motion path, dwell time, and nozzle distance. When recipes are stored and operator permissions are tiered, the process becomes easier to standardize across shifts.
Closed-loop recovery, sedimentation, and mist control
After impact, the slurry drains back into the recovery section. Reusable abrasive and water can be recirculated, while fines, broken media, and removed contaminants are separated through sedimentation, filtering, or waste handling steps. Closed-loop design reduces water loss and stabilizes operating conditions over longer runs.
Automatic waste-sand sedimentation and one-click discharge help reduce manual cleanup. This is especially useful in production environments processing carbide fines, metallic debris, scale, or coating residues. Because water mist can still be generated around the cabinet, effective extraction remains important even though airborne dust is far lower than in dry blasting.
Why pressure control matters
Blasting pressure should not be treated as a single setpoint with no feedback. In advanced systems, PID closed-loop control helps maintain constant slurry pressure despite hose losses, nozzle wear, viscosity change, or different part loading conditions. That stability improves surface uniformity and reduces variation between the first part and the hundredth part in the same production run.
| Parameter | Typical wet blasting range or note | Why it matters |
|---|---|---|
| Working pressure | Typically application-dependent, often from gentle finishing to moderate cleaning intensity | Sets impact energy and removal aggressiveness |
| Slurry concentration | Typical solids loading selected by material, finish target, and media shape/size | Controls cutting rate and finish consistency |
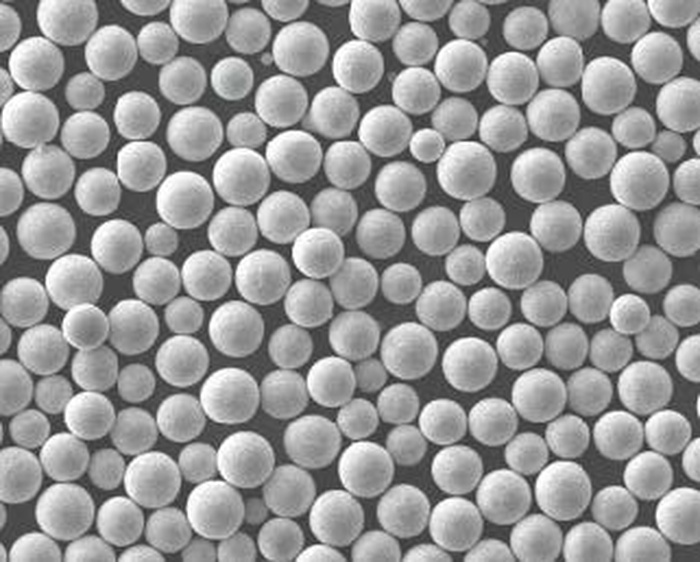
| Abrasive particle size | Commonly fine to medium grades; exact PSD chosen for deburring, honing, cleaning, or frosting | Influences Ra, edge rounding, and local aggressiveness |
| Compressed air flow | Sized to nozzle diameter, pressure target, and duty cycle | Affects acceleration stability and throughput |
| Nozzle standoff distance | Typically controlled within a narrow process window | Strong effect on pattern size and removal rate |
| Media consumption | Lower visible fugitive loss than dry blasting, but depends on breakdown rate and contamination | Drives operating cost and maintenance frequency |
| Motion/control system | Manual, indexed, or servo-controlled; recipe-managed systems offer higher repeatability | Determines precision and batch-to-batch consistency |
| Recovery loop | Recirculation with sedimentation, filtration, and mist extraction | Supports cleanliness, uptime, and environmental control |
wet blasting vs Dry Blasting vs Other Methods
Process selection should begin with the required outcome, not with the machine category. Wet blasting is not automatically superior to dry blasting, shot peening, or vibratory finishing; it is simply better aligned with certain combinations of substrate, geometry, cleanliness, and finish requirements.
Dry blasting remains effective for aggressive cleaning and high-removal jobs, especially when water is undesirable. Shot peening is different again because the objective is residual compressive stress rather than cosmetic or deburring finish. Vibratory finishing can be economical for bulk parts, but it is less selective and can struggle with localized features, hidden zones, or edge-specific treatment.
| Evaluation factor | wet blasting | Dry blasting | Shot peening | Vibratory finishing |
|---|---|---|---|---|
| Dust generation | Low airborne dust due to water phase | High unless heavily contained and extracted | Moderate; depends on enclosure and media | Low external dust, but compound/sludge handling required |
| Finish character | Fine, even, satin to matte; controlled micro-erosion | More aggressive texture; can be less uniform on delicate parts | Dimpled peened surface aimed at stress benefit | Smoothed mass finish; less directional control |
| Media embedding risk | Generally lower on many sensitive surfaces | Higher risk on some soft/coated substrates | Media contact is intentional and repeated | Not a blasting process; different contact mechanism |
| Precision/local selectivity | High when paired with fixturing or servo motion | Moderate to high, but more difficult on delicate surfaces | Moderate; focused on peening coverage | Lower for selective features |
| Burr removal capability | Good for fine burrs and controlled edge conditioning | Good for larger burrs but more aggressive | Not primarily a deburring process | Good for bulk small-part deburring |
| Surface cleanliness after process | Good when rinsing and recovery are well managed | Good, but dust and residual media cleanup can be greater | Good with controlled media condition | Good, though compound residue may need washing |
| Environmental profile | Better dust containment; requires slurry/waste handling | More dust management burden | Requires media management and enclosure control | Requires wastewater/sludge management |
| Best-fit use case | Precision finishing, honing, pretreatment, AM post-processing | Heavy cleaning, rust/scale removal, aggressive texturing | Fatigue-life enhancement by compressive stress | Bulk finishing of simpler small parts |
For formal vocabulary around blasting and peening, the ASTM terminology framework is useful because it separates process intent, media behavior, and verification language. For measurement and process capability thinking, many manufacturers also reference NIST metrology guidance when defining repeatability, uncertainty, and production control.
Key Specifications to Evaluate Before Buying
Buying wet blasting equipment should start with application physics, then move to machine architecture. A cabinet that works well for single-piece deburring may be the wrong choice for plate-shaped components, long cylindrical stock, or automated edge honing.
Pressure stability is more important than peak pressure
Buyers often focus first on the maximum pressure rating, but stable pressure within the real operating band is usually more important. If the application is precision deburring or edge preparation, consistency of delivered slurry energy matters more than having the highest nominal pressure on the nameplate.
Motion, fixturing, and nozzle path determine precision
Machine precision is not only about servo resolution. It also depends on fixture repeatability, nozzle wear monitoring, axis rigidity, rotary positioning, and the ability to store proven recipes. If the process target is a narrow edge radius or repeatable cosmetic finish, path control becomes a key specification.
Throughput depends on workflow, not only nozzle size
Throughput is shaped by loading method, chamber layout, recovery time, rinse/dry stages, recipe switching, and waste discharge intervals. A larger nozzle may remove material faster, but it can also consume more air, widen the blast pattern, and reduce control on small parts.
Utility and maintenance burden should be quantified early
Utilities include compressed air, electrical power, water management, drainage, and mist extraction. Maintenance includes pump wear parts, nozzle replacement, seals, media replenishment, sediment removal, and HMI/control support. These should be mapped before layout approval, not after installation.
Common buying checkpoints include:
- Required finish outcome: deburring, honing, cleaning, texturing, peening, or pretreatment.
- Substrate and hardness: carbide, steel, stainless, aluminum, glass, ceramic, or mixed materials.
- Workpiece geometry: simple flat parts, blind areas, slots, cylindrical bars, or complex multi-face shapes.
- Production mode: R&D, job-shop flexibility, batch production, or inline integration.
- Validation method: visual standard, roughness value, edge radius, weight loss, coating adhesion, or process capability.
In coating-related applications, the preparation stage should be aligned with the downstream coating system rather than treated as a standalone cleaning step. A combined workflow may involve blasting, rinsing, chemical treatment, and drying, which is why some users evaluate both blasting machines and integrated line concepts such as coating pretreatment wet blasting or combined PH14000 wet blasting phosphating equipment where the production context supports it.
When the application is cutting-tool preparation, the process window is even narrower. Edge symmetry, K-factor control, and localized finish quality matter more than raw removal rate, so buyers should evaluate dedicated process capability for edge honing of cutting tools rather than relying on generic blasting claims.
Applications Across Industries
Wet blasting is unusually broad in application because it can be tuned from gentle surface conditioning to moderate cleaning and deburring. The same process family appears in tool manufacturing, precision metalworking, additive manufacturing, glass finishing, and pre-coating lines, but each sector emphasizes a different performance metric.
In carbide tooling, the priority is controlled edge preparation. Manufacturers use wet blasting to create a stable edge radius and improve coating readiness without the uncontrolled chipping that can occur in harsher methods. In fabricated metal parts, the emphasis shifts toward selective burr removal, cosmetic consistency, and cleaning of machined surfaces.
For larger ferrous parts, wet blasting can remove scale or process residue while containing dust better than dry methods. In additive manufacturing, the process is useful for powder residue cleanup, support-mark blending, and smoothing of complex geometries that are difficult to finish mechanically. Electronics and glass applications prioritize appearance, tactile feel, and consistency of the final matte effect.
| Application | Industry served | Typical workpiece | Main process benefit |
|---|---|---|---|
| Edge honing | Carbide cutting tools | Inserts, drills, end mills | Controlled edge radius, better coating readiness, improved edge consistency |
| Burr removing | Precision metalworking | Stamped, machined, or sintered metal parts | Selective burr reduction with less distortion than aggressive dry methods |
| Scale removal | Forging and steel processing | Bars, forgings, heat-treated components | Cleaner surface with reduced airborne dust |
| Coating pretreatment | Painting and protective coatings | Steel, aluminum, fabricated assemblies | Improved cleanliness and anchoring condition before coating |
| AM post-processing | Additive manufacturing | Metal 3D-printed components | Powder residue cleanup and surface smoothing on complex shapes |
| Peening/conditioning | Metal fatigue-sensitive parts | Springs, formed parts, selected structural details | Surface conditioning with controlled impact exposure |
| Glass frosting | Glass processing | Panels, decorative components, technical glass | Uniform matte appearance and controlled translucency |
| 3C device finishing | Consumer electronics supply chain | Housings, frames, covers | Consistent cosmetic texture and smooth touch feel |
Application fit also depends on geometry. Flat or plate-shaped parts benefit from different handling than rod stock or highly contoured components. For example, production planners evaluating selective deburring may compare general cabinets with application-focused setups used for burr removing of metal parts to verify whether the machine path, fixture design, and media choice match the real defect pattern.
Equipment Selection Guide
Equipment selection should match production scale, part geometry, and control requirement. The best machine for R&D is usually not the best machine for a stable high-volume line, and the best machine for single-piece processing may be inefficient for flat parts or round stock.
A practical way to choose is to screen options by five filters: part size, part family variety, automation level, precision requirement, and target throughput. Only after that should buyers compare enclosure size, recovery design, and operator interface.
| Configuration / model tier | Target production scale | Workpiece size range | Precision level | Recommended applications |
|---|---|---|---|---|
| R&D robot-assisted flexible cell | Trials, sampling, frequent changeovers | Small to medium parts with varied geometry | High | Process development, sample testing, small-batch validation |
| Manual lab cabinet | Low-volume technical work | Small parts | Medium to high | Feasibility studies, repair work, parameter screening |
| Standard single-chamber batch cabinet | Stable batch production | Small to medium parts | Medium | General deburring, cleaning, edge prep |
| Single-piece dedicated machine | Repetitive part families | One part or fixture set at a time | Medium to high | Controlled single-part blasting, visual finish consistency |
| Double-chamber production system | Higher throughput batch production | Small to medium parts | Medium | Continuous loading rhythm, reduced idle time |
| Servo multi-axis complex-part system | Precision production | Complex 3D parts | High | Multi-face finishing, selective treatment, edge-specific blasting |
| Plate-part large-workspace machine | Medium to large flat components | Plate-shaped or wide parts | Medium | Flat-part pretreatment, cosmetic finishing, panel processing |
| Round-rod or bar-stock line | Continuous long-part processing | Cylindrical rods, bars, shafts | Medium | Scale removal, conditioning of long cylindrical workpieces |
For R&D and mixed-part development, a flexible cell such as the RB-6 robot-type wet blasting equipment fits projects where part geometry changes often and process discovery matters more than raw throughput. By contrast, a standard batch environment may align more naturally with an SC-40 single-chamber wet blasting cabinet when the workpiece family is stable and loading rhythm is predictable.
If production is organized around one workpiece at a time, a dedicated SP1580 single-piece wet blasting machine can simplify handling and improve consistency. For planners focused on takt time reduction in batch operations, the DC-40 double-chamber wet blasting system is more relevant because chamber architecture influences loading overlap and effective machine utilization.
Cost, Lead Time and ROI Considerations
Wet blasting project cost is driven less by the base cabinet alone and more by the final process package. Price typically moves with chamber size, motion-axis count, recovery system complexity, pump and nozzle specification, abrasive compatibility, control architecture, and whether the machine must integrate with upstream or downstream equipment.
Automation is one of the largest cost multipliers. Manual or semi-automatic systems can be effective for flexible low-volume work, but servo motion, recipe management, robotic loading, interlocks, and traceability raise the investment level while usually improving consistency. Buyers should separate “must-have” process controls from “nice-to-have” automation features to avoid paying for unused complexity.
Abrasive system design also affects ownership cost. Media breakdown rate, contamination sensitivity, sediment removal effort, and the frequency of concentration correction all shape the real operating expense. Machines that simplify waste-sand discharge and reduce mist-related housekeeping can lower labor burden even if their initial price is higher.
Lead time should be treated as typical, not absolute. Standardized cabinets may ship faster than custom multi-axis cells, while process-validated projects involving fixtures, sample approval, electrical adaptation, or integrated pretreatment steps may take longer. In many industrial purchases, the practical schedule includes quotation, sample verification, design freeze, manufacturing, factory acceptance, shipment, installation, commissioning, and operator training rather than just machine assembly time.
ROI analysis is strongest when linked to a measurable production pain point. Common value drivers include:
- labor reduction versus manual deburring or hand finishing;
- improved coating adhesion and reduced rework in pretreatment lines;
- longer tool life when edge honing is controlled rather than inconsistent;
- lower scrap from over-blasting, under-blasting, or cosmetic rejection;
- cleaner work environment and reduced dust-management burden compared with dry blasting;
- faster qualification of new part programs through stored process recipes.
A useful ROI model compares current-state cost per acceptable part with future-state cost per acceptable part. That model should include operator time, abrasives, utilities, maintenance, cleaning, scrap, rework, and downtime. It should also account for the quality effect: a process that removes one manual station but creates more variation is not necessarily a true improvement.
For procurement teams, the most important caution is to avoid using generic “price per machine” comparisons between unlike systems. Wet blasting value comes from process fit, recovery stability, and repeatable quality output, not from enclosure size alone.
Why Choose DassiAuto — Our Company
DassiAuto Intelligent Equipment Co., Ltd is a Chinese manufacturer established in 2012 and focused on industrial wet blasting technology for surface treatment. According to the company context, it operates as a national high-tech enterprise under the ISO 9001 quality management standard and holds invention patents, utility model patents, and software copyrights related to blasting equipment and control systems. Its stated scope covers planning, design, manufacturing, sales, and application development across wet blasting equipment and matched abrasive systems.
From an engineering standpoint, the company’s wet blasting platform is defined by slurry-based abrasive delivery, PID closed-loop pressure control, servo-driven X/Y/Z linkage, HMI recipe management with hierarchical permissions, automatic waste-sand sedimentation with one-click discharge, and dust-collection arrangements intended to reduce water mist. The equipment range covers eight configurations spanning R&D, batch production, and application-specific processing, including tool edge honing, metal-part deburring, scale removal, coating pretreatment, AM post-processing, peening, glass frosting, and 3C finishing. The stated customer references include Wecan Cutting Tools, Ruian Carbide Tools, Huareal, Metcera, OKE, YG, Kelite, and XTC.
Operationally, the company describes a full-cycle model from sample testing to after-sales, including application development, planning, design, manufacturing, installation, commissioning, training, spare parts, abrasive resupply, and process optimization. Its corporate background and certification profile are summarized on the about DassiAuto page, which aligns with the role of a process-focused equipment manufacturer rather than a reseller.
FAQ
Q1. Can wet blasting be tested on my parts before I buy a machine?
Yes. In industrial procurement, sample testing is a standard way to confirm finish level, burr-removal behavior, edge radius, and media suitability before a machine configuration is finalized. It is especially important when the part material, geometry, or cosmetic requirement is sensitive to nozzle angle, slurry concentration, or dwell time.
Q2. Is wet blasting suitable for both small precision parts and larger production components?
Generally, yes, but the machine architecture must match the part family. Small precision parts may need tight fixturing and servo path control, while larger components may need bigger work envelopes, stronger recovery loops, or dedicated handling for flat parts, rods, or heavy forgings.
Q3. How do I choose the right abrasive for wet blasting?
Abrasive choice depends on substrate hardness, target finish, burr size, edge condition, allowable removal rate, and cost target. Buyers should evaluate particle size distribution, media hardness, shape, breakdown behavior, and contamination risk rather than selecting solely by nominal grit number.
Q4. What installation and operator training are usually required?
Most systems require compressed air, electrical supply, water management, drainage planning, and safe access for maintenance. Training typically covers recipe setup, pressure adjustment, media management, nozzle wear inspection, cleaning routines, and recovery-loop maintenance so that operators can keep the process stable over time.
Q5. How long does it usually take to receive a wet blasting machine?
Lead time varies by whether the project uses a standard cabinet, a custom fixture package, or a more automated multi-axis cell. Buyers should evaluate the full timeline from application review and sample approval through manufacturing, shipment, installation, commissioning, and validation rather than focusing only on assembly duration.
Q6. What after-sales support matters most for wet blasting equipment?
The most important support items are spare parts availability, abrasive supply continuity, process troubleshooting, and remote or on-site help when finish results drift. In practice, long-term performance depends as much on stable consumables and parameter support as on the original machine build.